








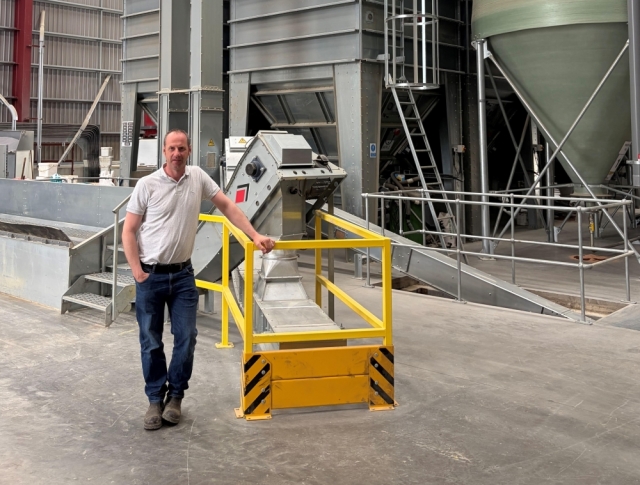
McArthur BDC has designed and installed an integrated feed processing and storage system for Duncan Farms, a Scottish family farming business producing over five million eggs per week, reducing labour requirements and improving operational efficiency.
The new system features 12 hopper bottom silos, each with a capacity of 65 cubic metres, linked by a network of conveyors and controlled via a 21-inch PLC touchscreen with remote access functionality.
“We had long recognised some inefficiencies in our feed mixing operations,” said Duncan Gray of Duncan Farms, who managed the project. “The difference the new system has made is significant. We’ve reduced labour requirements, saved time and improved overall efficiency across the operation.”
System design
The plant includes three intake points – one for bought-in ingredients such as sunflower pellets and soya meal, and two for home-grown wheat and barley stored in adjacent buildings with a combined capacity of 17,000 tonnes. The PLC-controlled feed system allows all 12 silos to be filled from any intake.
Each silo is fitted with high, mid and low-level sensors to automate filling and emptying, while vibratory motors ensure efficient clean-out. The Duncan Farms feed processing system is designed with future expansion in mind.
“We liked McArthur BDC‘s practical, problem-solving approach,” Gray added. “They delivered a professional service from start to finish.”